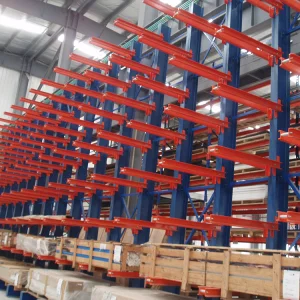
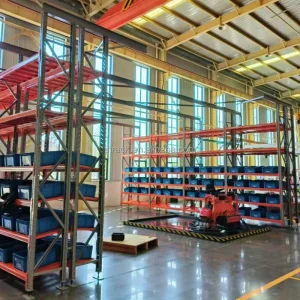
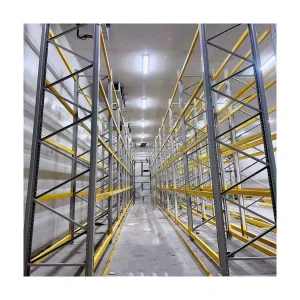
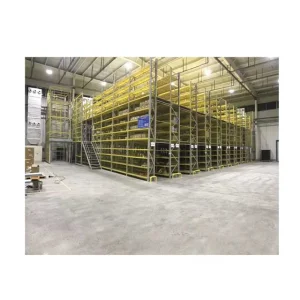
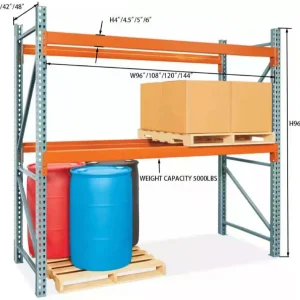
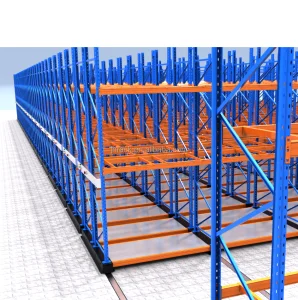
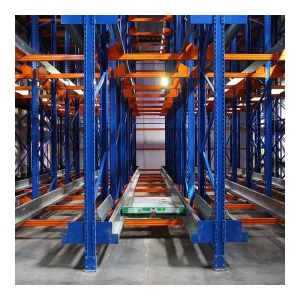
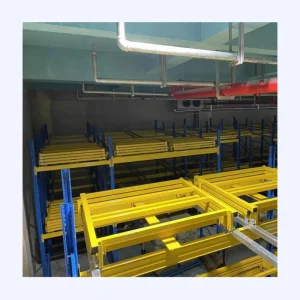
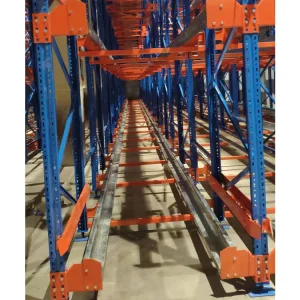
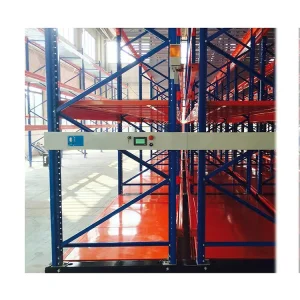
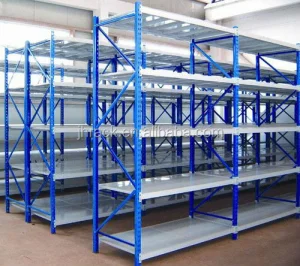
In today's high-velocity industrial environment, mobile shelving represents the nexus of space efficiency and operational agility. As a premier manufacturer, Jinhui Storage Equipment integrates smart-automation with heavy-duty structural integrity.
Global corporations face increasing warehouse costs. Our mobile shelving solutions offer 100% access while reducing floor footprint by up to 50%. Whether for cold chain logistics or archival storage, we implement bespoke technical roadmaps tailored to regional building codes (ASTM/FEM/ISO compliance).
Our R&D team is pioneering the shift towards automated mobile rack systems featuring IOT connectivity, remote monitoring, and safety-first sensor integration. By digitizing the warehouse, we help clients track inventory movement in real-time, effectively bridging the gap between hardware and software intelligence.
We combine ISO 9001 quality management with 14 years of rigorous performance data, ensuring every unit meets seismic and load capacity mandates.
Yes, with 68 R&D engineers, we execute over 120+ custom projects annually, providing full-cycle technical support from layout design to site installation.
Our engineering team analyzes local regional regulations (e.g., North American RMI, European EN standards) during the preliminary design phase.
 Jinhui Storage Equipment