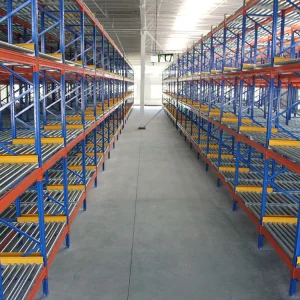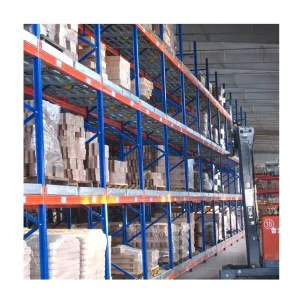
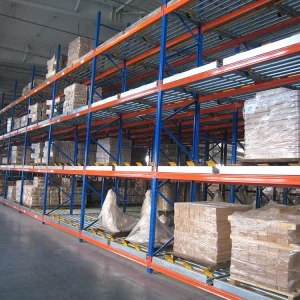
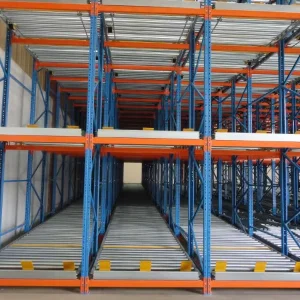
Moundou, as the economic heartbeat and primary industrial center of Chad, is experiencing rapid commercial expansion. Driven by agricultural processing, cotton manufacturing, brewing, and regional logistics distribution, modern enterprises in Moundou face escalating demands for optimized floor space utilization and high-density inventory management. Traditional selective pallet racking often falls short in storage density, making advanced Pallet Flow Racking systems essential for modern Moundou warehouses seeking First-In, First-Out (FIFO) inventory control and maximum throughput.
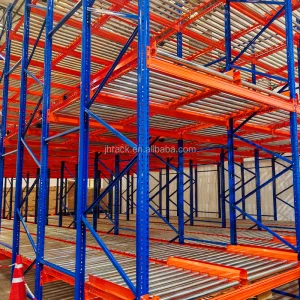
Globally, the industrial storage sector has transitioned towards automated, high-density, and gravity-driven architectures. Dongguan Jinhui Storage Equipment Co., Ltd. bridges the gap between state-of-the-art Chinese manufacturing and the burgeoning industrial needs of Moundou. By utilizing incline roller tracks and gravity deceleration brakes, our pallet flow solutions allow pallets to move smoothly from the loading aisle to the picking face, slashing forklift travel times by up to 75% and recovering up to 60% of floor space compared to conventional selective setups.
Dongguan Jinhui Storage Equipment Co., Ltd. is a professional manufacturer specializing in warehouse storage solutions and industrial racking systems in China. Since its establishment in 2017, the company has been dedicated to providing high-quality storage equipment for warehouses, factories, logistics centers, supermarkets, and distribution facilities worldwide.
Our manufacturing facility covers over 18,600 square meters, equipped with advanced automatic production lines, precision laser cutting machines, CNC punching equipment, robotic welding systems, and powder coating lines. With strict production management and continuous innovation, we provide reliable and cost-effective storage solutions for customers across different industries.
Jinhui offers a comprehensive range of products including selective pallet racks, heavy-duty warehouse racking, longspan shelving, mezzanine floor systems, drive-in racks, cantilever racks, mobile shelving, steel platforms, wire mesh containers, and customized storage solutions. Every product is designed to maximize warehouse efficiency, improve space utilization, and enhance operational safety.
With an annual export revenue of approximately USD 16 million, our products are exported to more than 50 countries and regions. We have accumulated 8 years of export experience and 14 years of industry experience, serving customers with professional technical support and efficient international trade services.
Quality is the foundation of our business. Our factory operates under a strict quality management system with ISO 9001 certification. Every production process is monitored carefully, and finished products undergo load capacity testing, dimensional inspection, coating thickness measurement, and welding strength inspection before shipment. Our professional quality control team consists of 46 experienced inspectors, ensuring consistent product quality and customer satisfaction.
Supported by over 980 supply chain partners, we maintain stable material sourcing and efficient production schedules, allowing us to deliver projects on time while maintaining competitive pricing.
Our major customers include warehouse solution distributors, logistics companies, industrial manufacturers, retailers, wholesalers, engineering contractors, and e-commerce fulfillment centers across Europe, North America, Southeast Asia, Australia, South America, and the Middle East.
Jinhui has established a strong research and development team with 68 R&D engineers, providing OEM & ODM customized solutions based on warehouse layout, load requirements, and operational needs. Last year, our engineering team successfully launched 126 new products and upgraded storage solutions, demonstrating our continuous commitment to innovation.
Driven by the philosophy of quality, innovation, and customer satisfaction, Dongguan Jinhui Storage Equipment Co., Ltd. strives to become a trusted global partner for warehouse storage systems, delivering durable products, professional service, and long-term value to customers around the world.
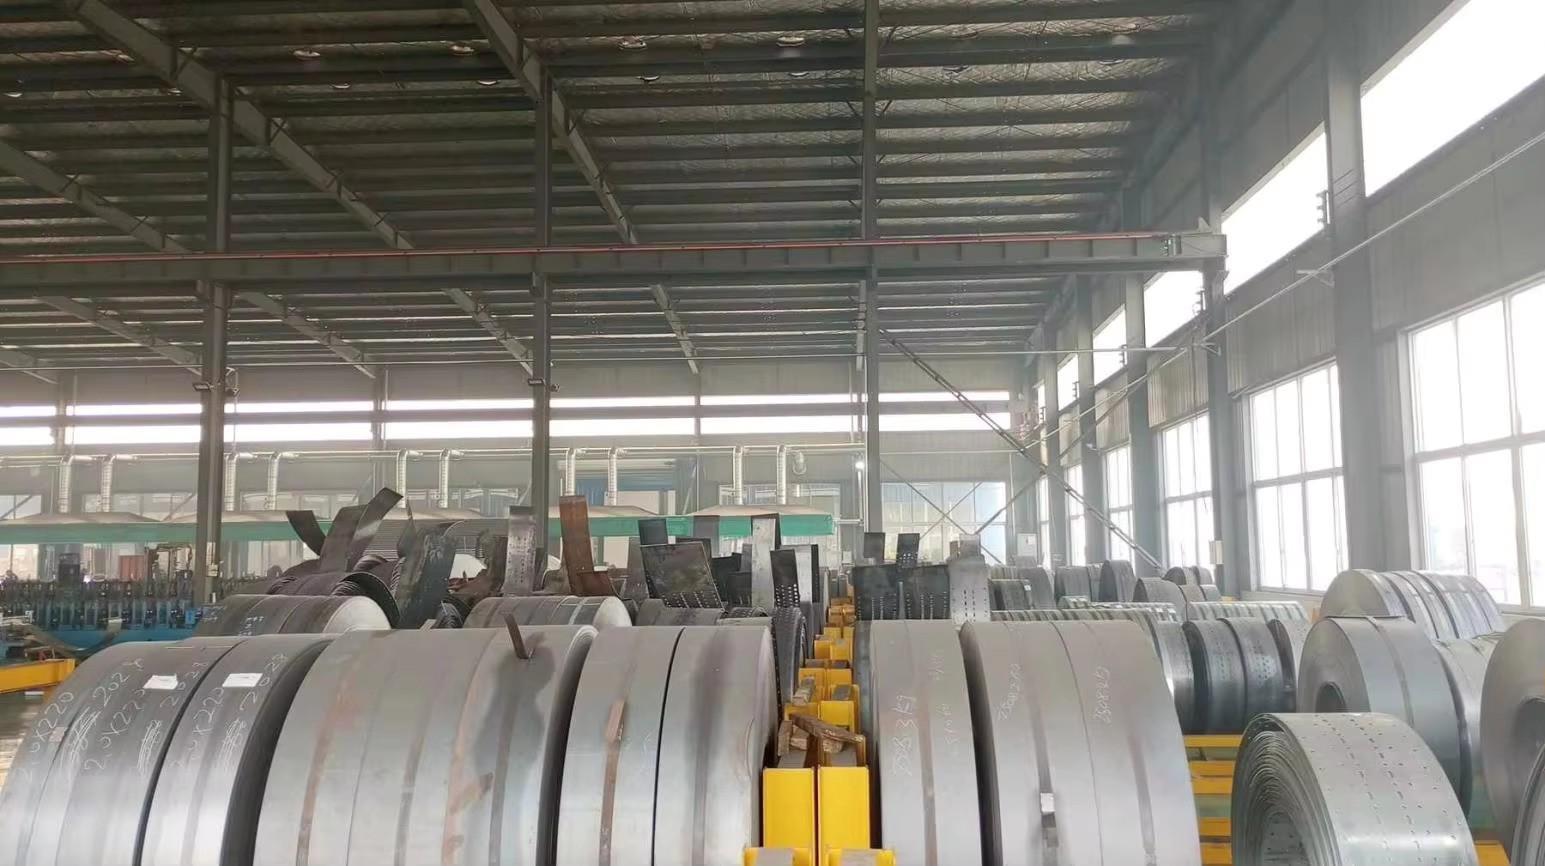
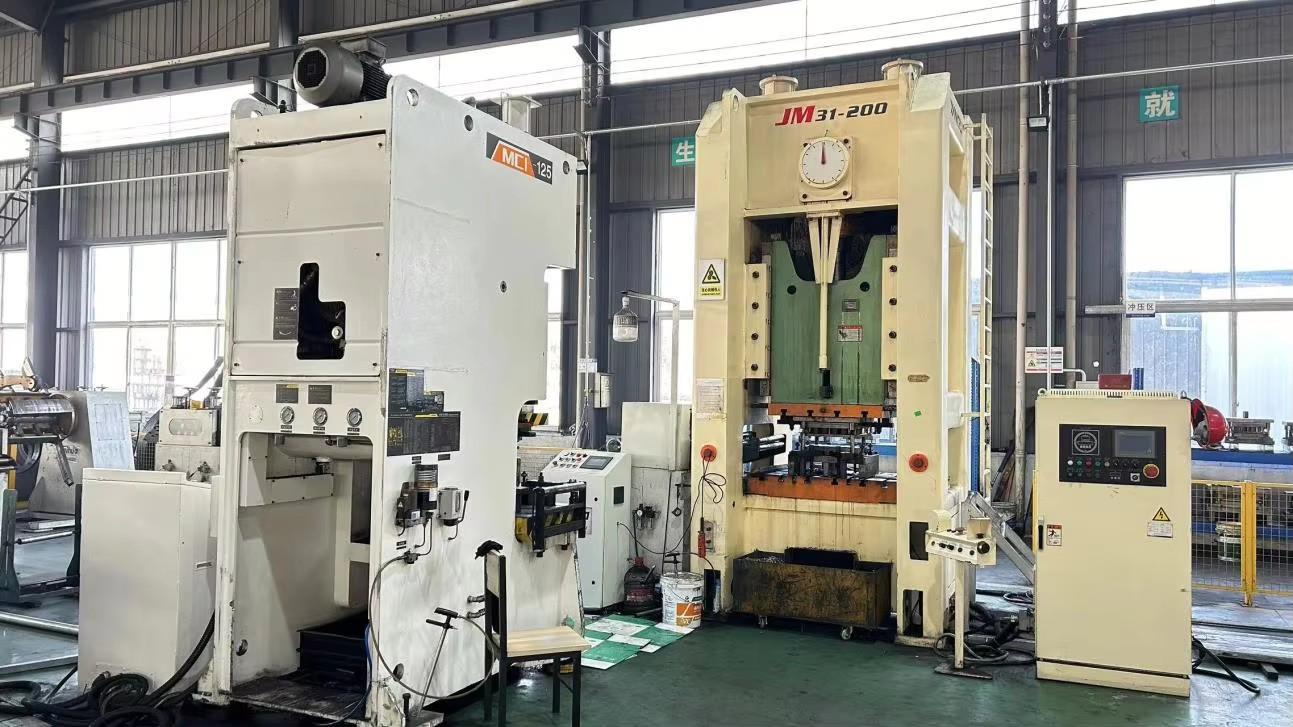
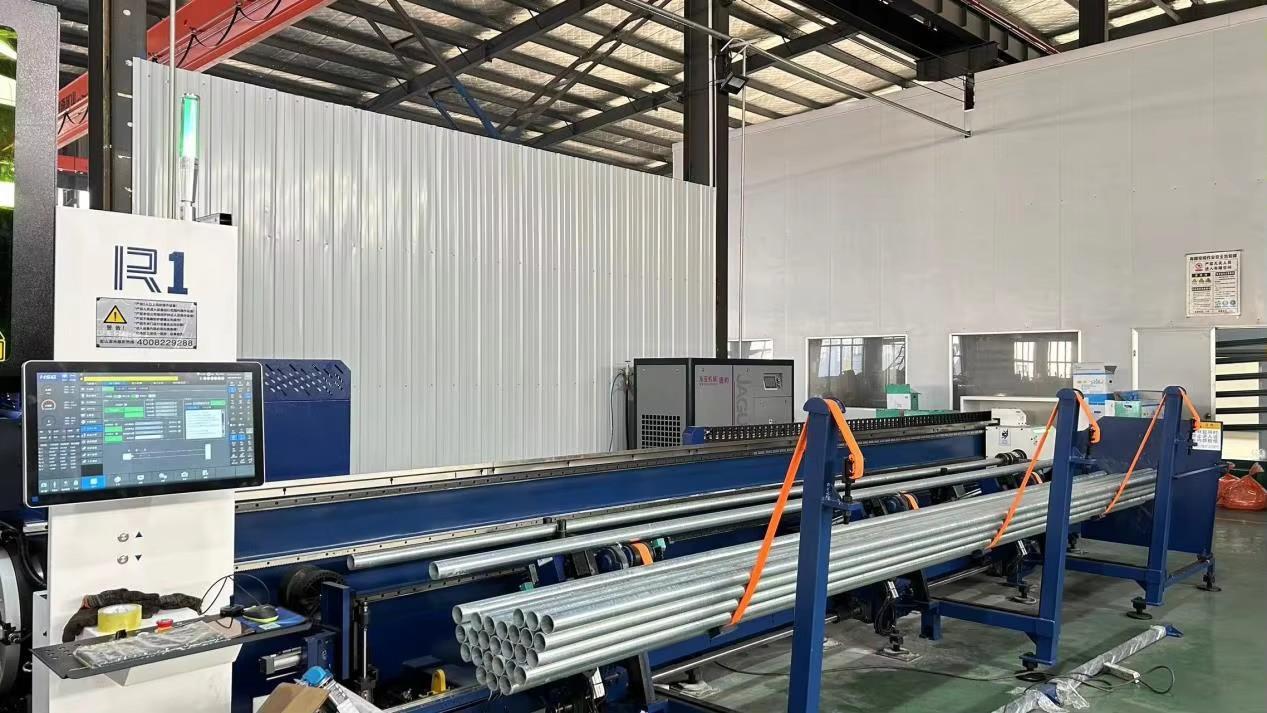
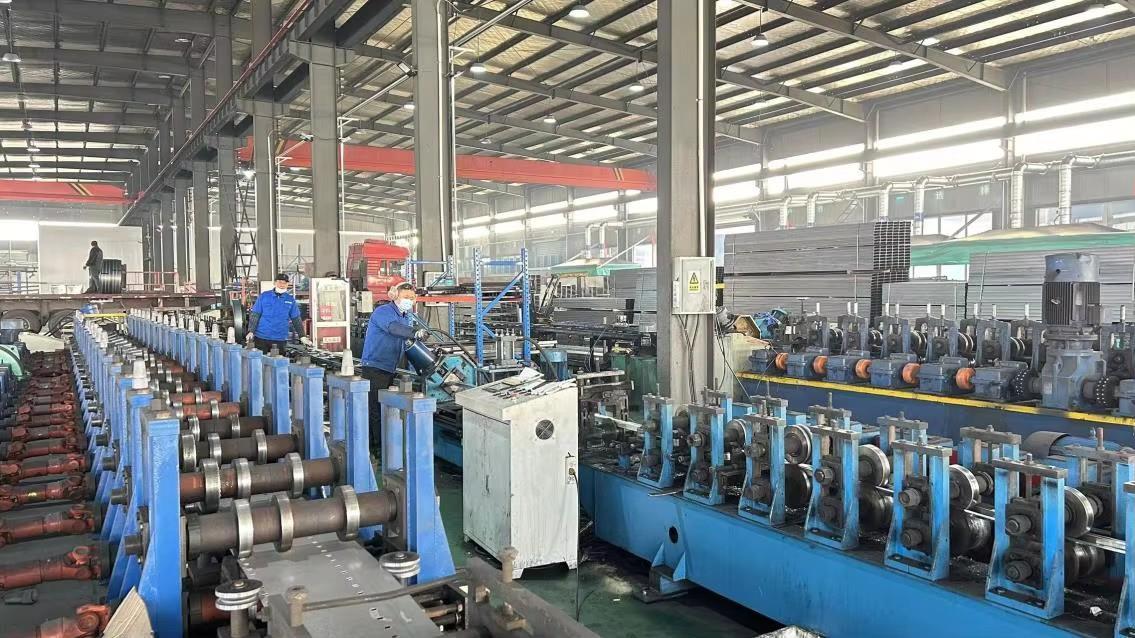
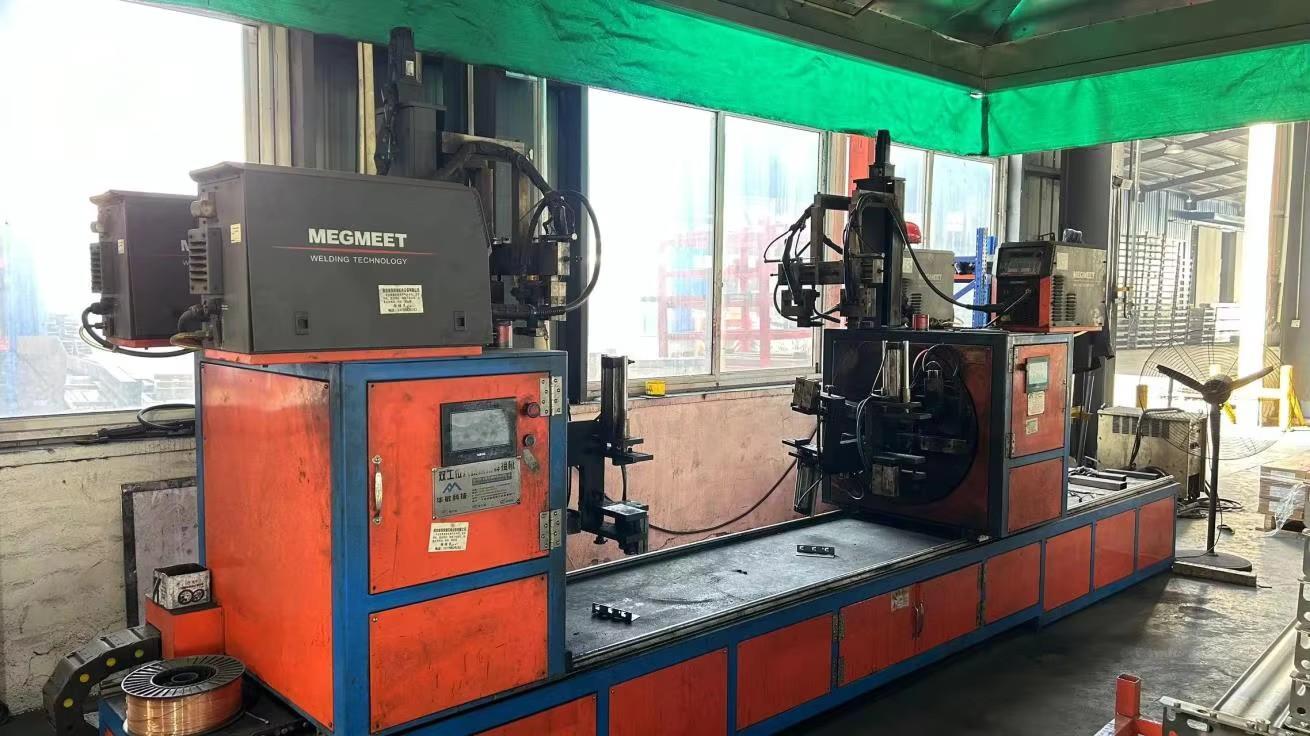
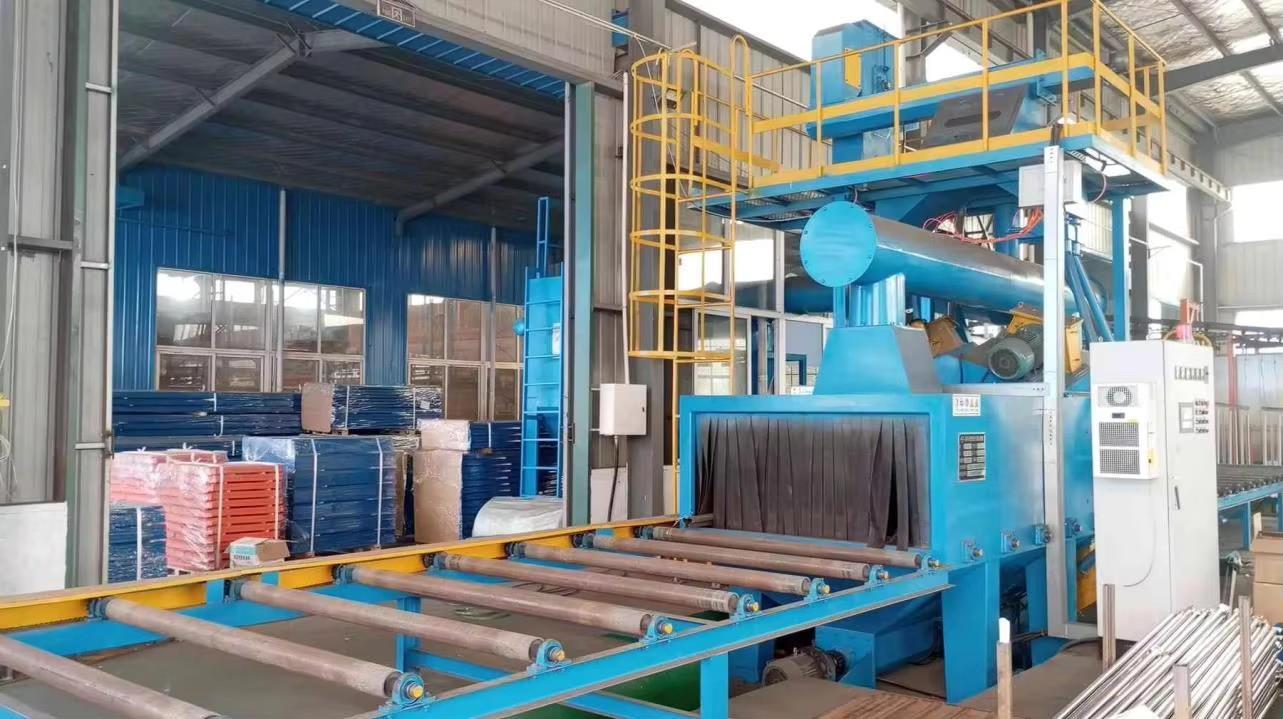
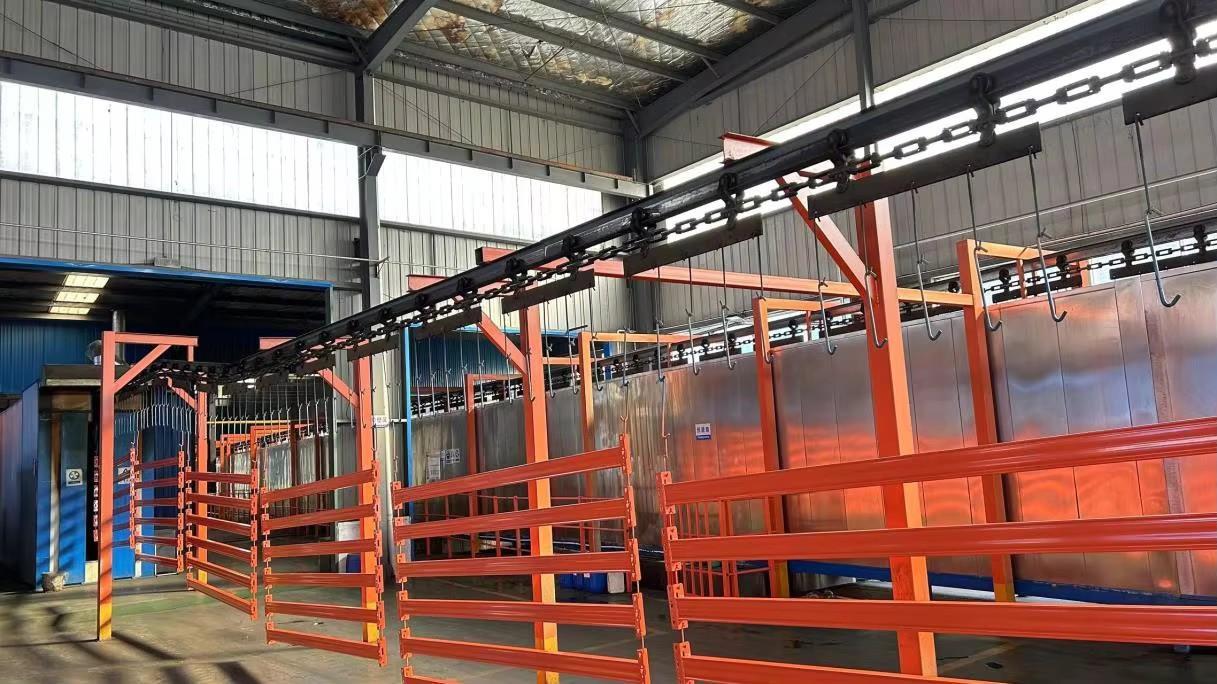
In Moundou’s dynamic industrial ecosystem, warehouse configurations must withstand unique operational environments. Our Pallet Flow Racking Systems are engineered with high-grade structural steel and anti-corrosion powder coatings designed to endure regional climate variations. Ideal application scenarios in Moundou include:
We provide end-to-end technical support, including customized CAD layout designs, seismic and load capacity calculations, and comprehensive installation manuals, ensuring complete structural safety and compliance with international standards (CE, ISO 9001).
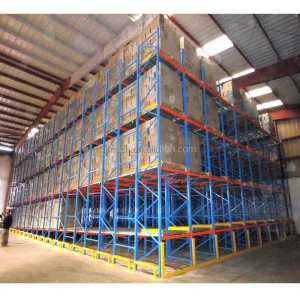
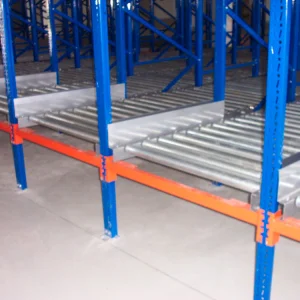
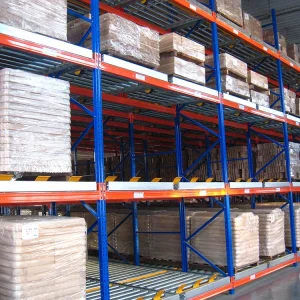
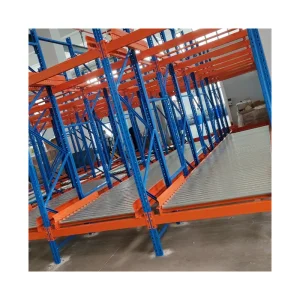
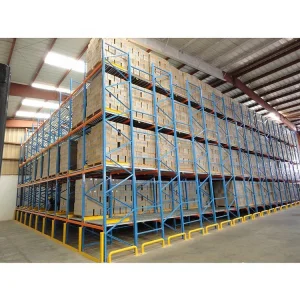
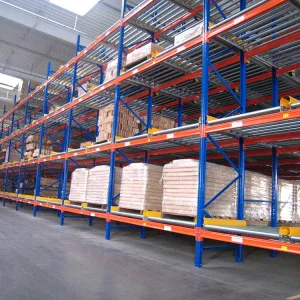
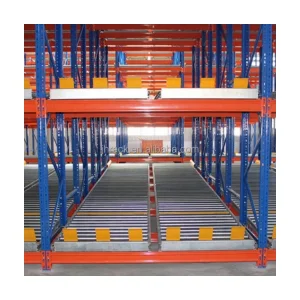
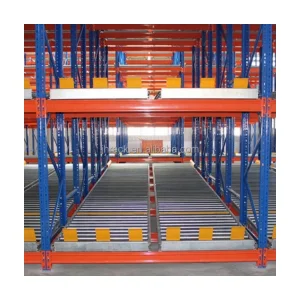
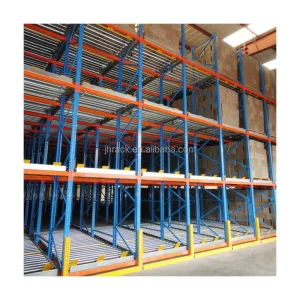
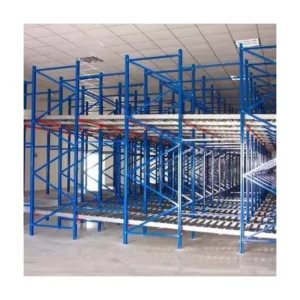
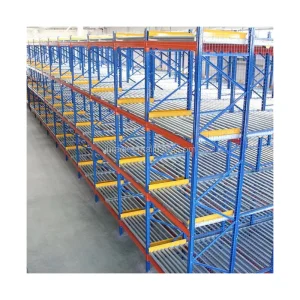
Pallet flow racks offer significantly higher storage density by utilizing gravity and rollers, eliminating multiple aisles and increasing usable warehouse capacity by up to 60% while supporting seamless FIFO (First-In, First-Out) inventory rotation.
Yes. We have over 8 years of professional export experience, providing robust packaging, corrosion-resistant coatings, and complete structural documentation tailored to international freight and local climatic requirements in Moundou.
Every racking system is manufactured under ISO 9001 certified protocols, utilizing high-grade steel subjected to rigorous load capacity testing, dimensional inspection, and weld strength evaluation by our team of 46 quality control inspectors.
Absolutely. Our 68 R&D engineers specialize in OEM & ODM customized storage solutions, tailoring lane depths, tier heights, and roller brakes to match your precise warehouse dimensions and forklift specifications.
 Jinhui Storage Equipment